Project Overview and Application
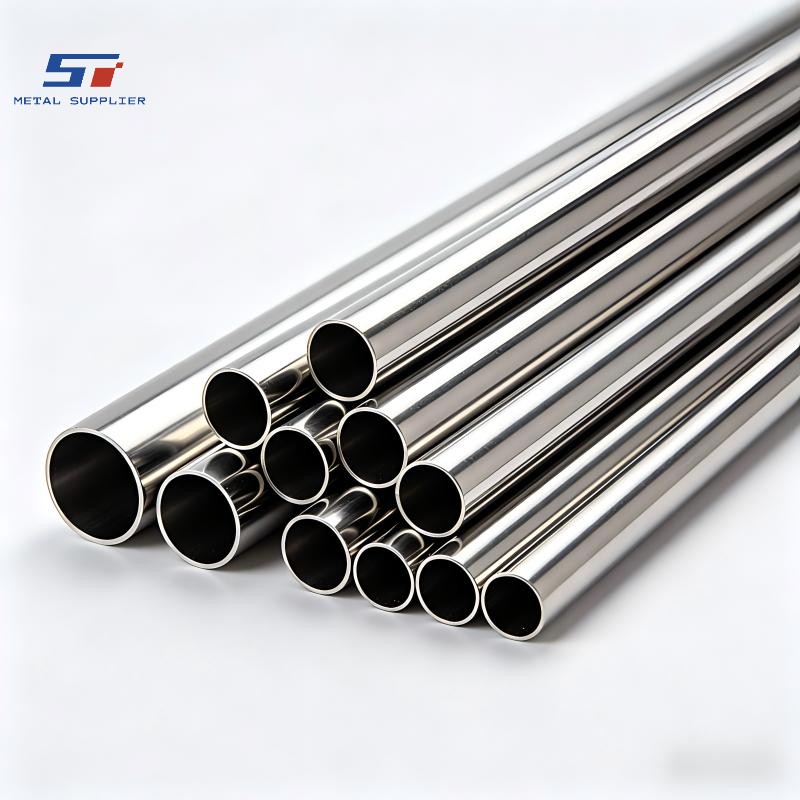
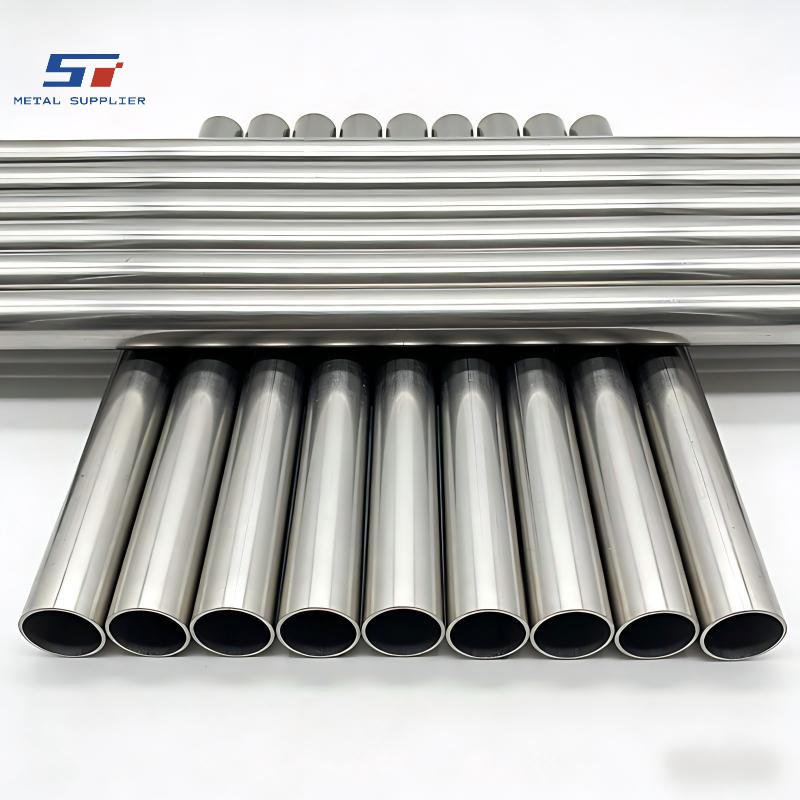
The technical requirements for a seamless alloy steel tube supply for a high-temperature boiler retrofit center on the critical balance between thermal stability and structural integrity. In industrial steam generation environments, the transition from aging infrastructure to modernized systems requires a precise understanding of how alloyed materials respond to sustained thermal stress. The supply of seamless alloy steel tubes for such projects is not merely a matter of delivery but a comprehensive exercise in material science, metallurgical verification, and project-specific logistics.
Application Context and Engineering Environment
High-temperature boiler systems operate under conditions that push the limits of conventional metallurgy. In a retrofit scenario, the objective is often to replace worn heating surfaces, superheaters, or headers with materials that offer improved creep resistance and oxidation stability. The environment typically involves high-pressure steam and flue gas temperatures that can fluctuate significantly during startup and shutdown cycles. For the supply of seamless alloy steel tubes, the context involves identifying the correct alloy grade—often chromoly variants such as T11, T22, or T91—that aligns with the existing boiler design while meeting modern safety standards. The engineering challenge is compounded by the need for these tubes to integrate seamlessly with older headers and support structures, necessitating tight tolerances on outside diameters and wall thicknesses. Furthermore, the operational environment often involves corrosive elements in the flue gas, which can lead to fireside corrosion if the material selection does not account for the specific fuel chemistry used in the boiler. Understanding the legacy design limits of the boiler is also essential to ensure the new materials do not induce unforeseen stresses on the surrounding structural components.
Technical Requirements and Material Challenges
The primary challenge in a high-temperature boiler retrofit is the prevention of premature material failure due to creep or graphitization. Creep is the tendency of a solid material to move slowly or deform permanently under the influence of persistent mechanical stresses at elevated temperatures. Requirements for the seamless alloy steel tubes include strict adherence to chemical composition limits, particularly for elements like chromium, molybdenum, and vanadium, which provide the necessary high-temperature strength and creep-rupture resistance. Beyond the chemistry, the physical state of the tubes is paramount. Any internal or external surface defects could serve as stress concentrators, leading to cracks under thermal cycling. Furthermore, the dimensional accuracy of the tube ends is vital for field welding. In many retrofit projects, the space for maneuvering is restricted, meaning the tubes must be supplied in exact lengths or with pre-beveled ends to reduce on-site machining time and potential contamination of the boiler internals. The material must also exhibit high ductility to accommodate the thermal expansion that occurs as the boiler reaches its operating temperature. The ability of the alloy to resist steam-side oxidation, which can lead to exfoliation and downstream turbine damage, is also a critical performance requirement for these high-alloy grades.
Material Selection and Specification Process
The selection process for the seamless alloy steel tubes starts with a thorough review of the boiler’s operating parameters, including peak pressure and temperature profiles. Standard carbon steel is often insufficient for the superheater or reheater sections, leading to the selection of ferritic alloy steels. These materials are chosen for their lower coefficient of thermal expansion compared to austenitic stainless steels, which helps minimize thermal fatigue at the points where the tubes are welded to carbon steel headers. The specification process also involves determining the required heat treatment—typically normalizing and tempering—to ensure a stable microstructure. This microstructure is essential for long-term service life, as it dictates how the steel will behave after thousands of hours of operation at temperatures exceeding 500 degrees Celsius. For instance, T91 is often preferred for its superior strength-to-weight ratio, allowing for thinner tube walls and improved heat transfer efficiency, although it requires much more stringent control during the welding and post-weld heat treatment phases.
Production Coordination and Scheduling
Coordination during the production of seamless alloy steel tubes for a retrofit requires close synchronization between the mill’s output and the installation timeline. Unlike new builds, retrofits often have a fixed shutdown window during which all work must be completed. The production sequence must prioritize the most critical sections, such as the high-pressure tubes that require more extensive testing. Throughout the manufacturing phase, the focus remains on maintaining a consistent heat-to-heat chemical profile. This consistency is crucial for the welding procedures that will be used on-site, as it ensures that the weldability of the entire batch of tubes is uniform. Regular updates on the production status are maintained to allow the project managers to adjust the arrival of mechanical contractors and specialized welding teams. The supply chain must also account for the potential need for emergency replacements, maintaining a small buffer of material that matches the project’s specific heat numbers to avoid delays in case of on-site damage during installation.
Quality Checkpoints and Technical Verification
Quality assurance for seamless alloy steel tubes in high-temperature applications involves a multi-stage verification process. Initial checks begin with the heat analysis of the raw steel billet. Once the tubes are formed through the seamless extrusion or piercing process, they undergo non-destructive testing (NDT). This typically includes ultrasonic testing to detect subsurface flaws and eddy current testing for surface integrity. For tubes destined for boiler retrofits, hydrostatic testing is also a standard requirement to verify that the tubes can withstand pressures well above their operating limit. Additionally, hardness testing is performed to confirm that the heat treatment has achieved the desired mechanical properties. Positive Material Identification (PMI) is a critical checkpoint performed just before shipment to ensure that every individual tube matches the required alloy grade. Every step of this verification is documented in a detailed Material Test Certificate (MTC), providing a transparent record of the material’s compliance with the relevant industrial standards such as ASME SA213 or EN 10216-2.
Production Coordination and Fabrication Integration
The integration of custom fabrication requirements into the production workflow is a key factor in the success of the boiler retrofit. Often, tubes must be bent to specific radii or swaged at the ends to fit into existing headers. These processes must be carried out under controlled conditions to avoid inducing residual stresses that could lead to premature failure in service. Cold-bending operations are followed by thermal stress relief if the deformation exceeds specified limits. The coordination team ensures that the fabricators are provided with detailed bending schedules and that the material’s grain structure is preserved through appropriate tooling and lubricants. This level of technical oversight extends to the marking and identification of each bent component, ensuring that they can be easily placed within the boiler’s complex tube bank layout.
Packaging, Preservation, and Site Delivery
The final stage of the project involves the careful packaging and delivery of the seamless alloy steel tubes to the retrofit site. Given the susceptibility of high-alloy steels to atmospheric corrosion if left unprotected, the tubes are often treated with a light coating of rust-preventative oil or a specialized varnish that does not interfere with subsequent welding. The ends of the tubes are fitted with heavy-duty plastic caps to protect the beveled edges from mechanical damage during transit and to prevent the ingress of moisture or debris. For boiler retrofits, where organization is key to a fast turnaround, the tubes are bundled and tagged according to their specific installation zone within the boiler. This systematic approach ensures that when the material arrives, the site team can immediately identify and move the necessary components to the work area, minimizing delays and maintaining the integrity of the alloy surfaces until the moment of installation. Additionally, shipping containers may be fitted with desiccant packs to control humidity during sea transit, further safeguarding the material against oxidation.
Contact Shengtao Metal for Steel Product Solutions
If you are looking for reliable steel and metal product solutions, feel free to send us your inquiry.
Simply provide your specifications such as material grade, dimensions, quantity or application, and our team will respond quickly with professional support and a competitive quotation.
Email: stsalesman4@stmetal001.com


Request A Quote
Scan to Wechat/Whatsapp :